Mould Making
Injection moulds designed, machined, fitted and maintained by the team that also runs the press.
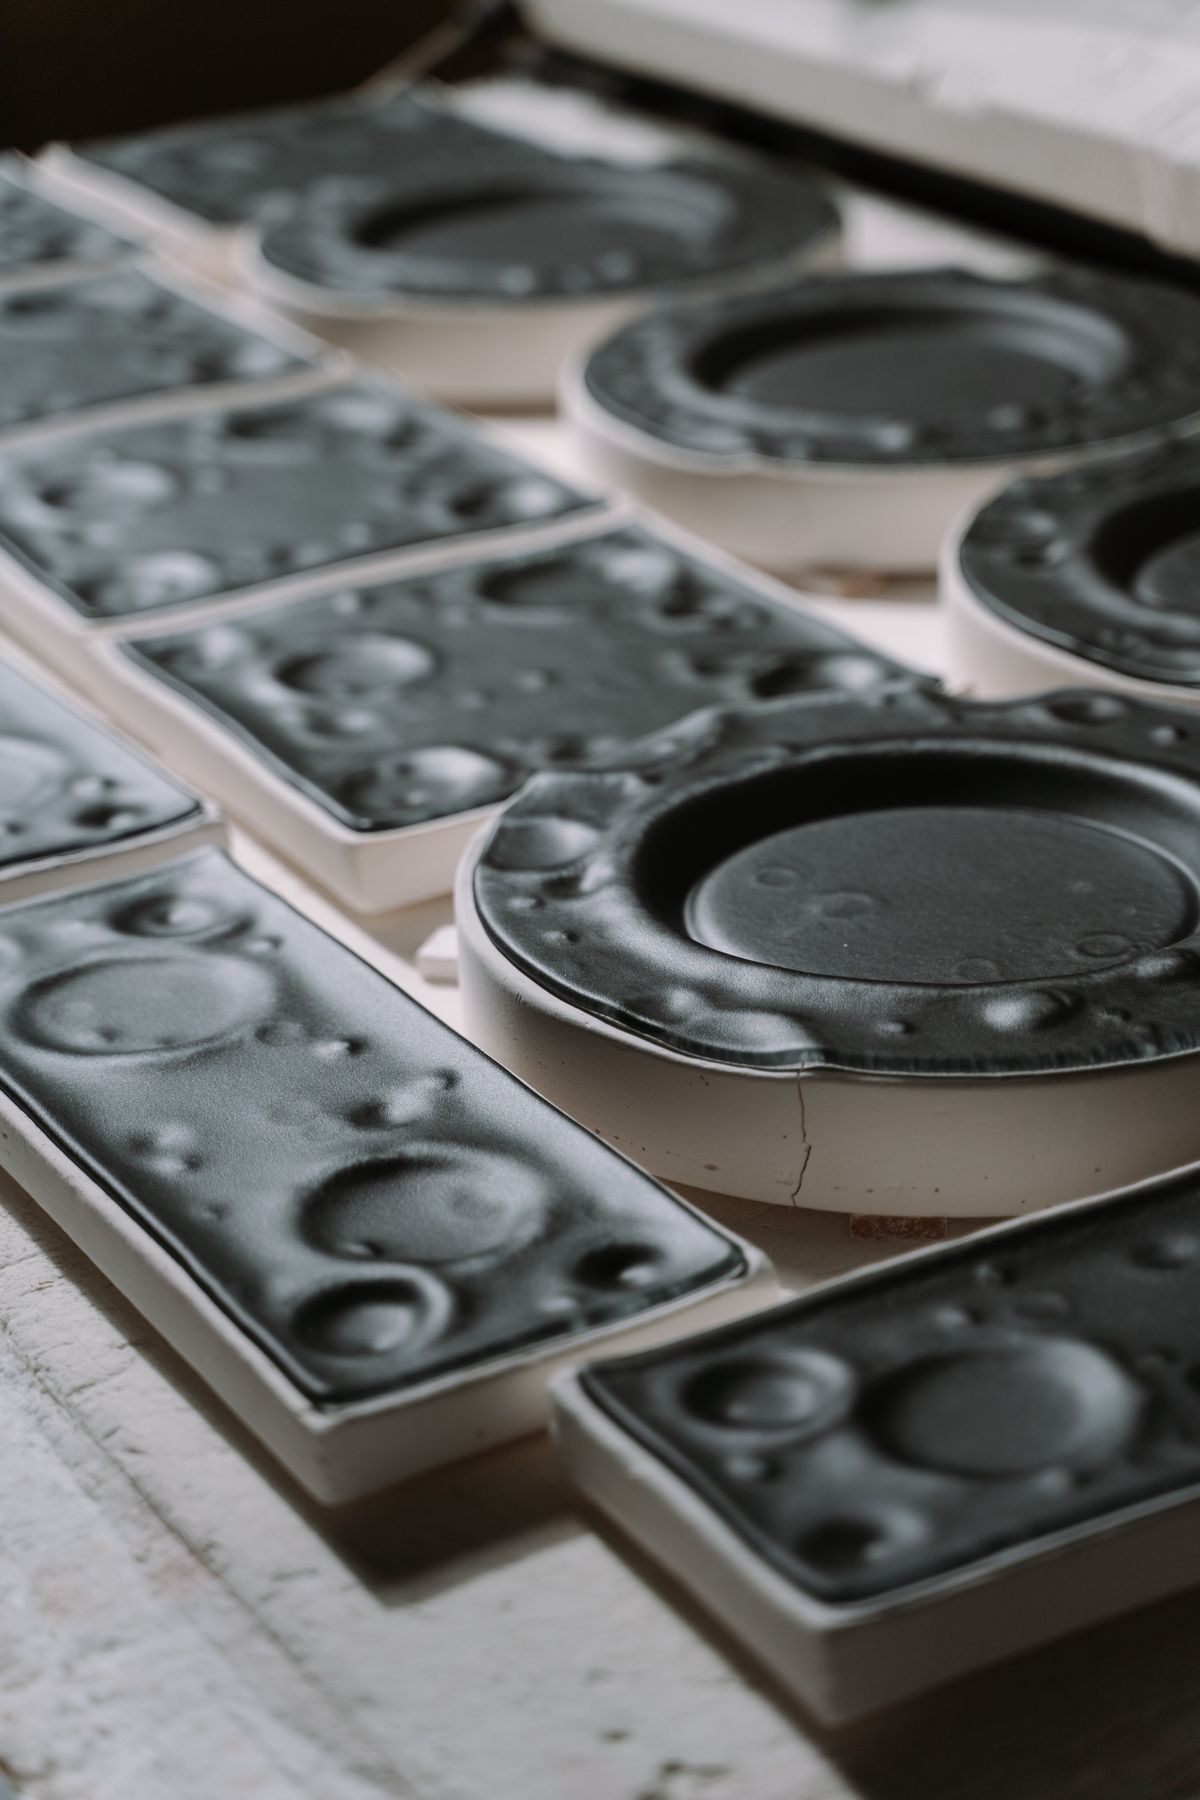
Injection moulds designed, machined, fitted and maintained by the team that also runs the press.
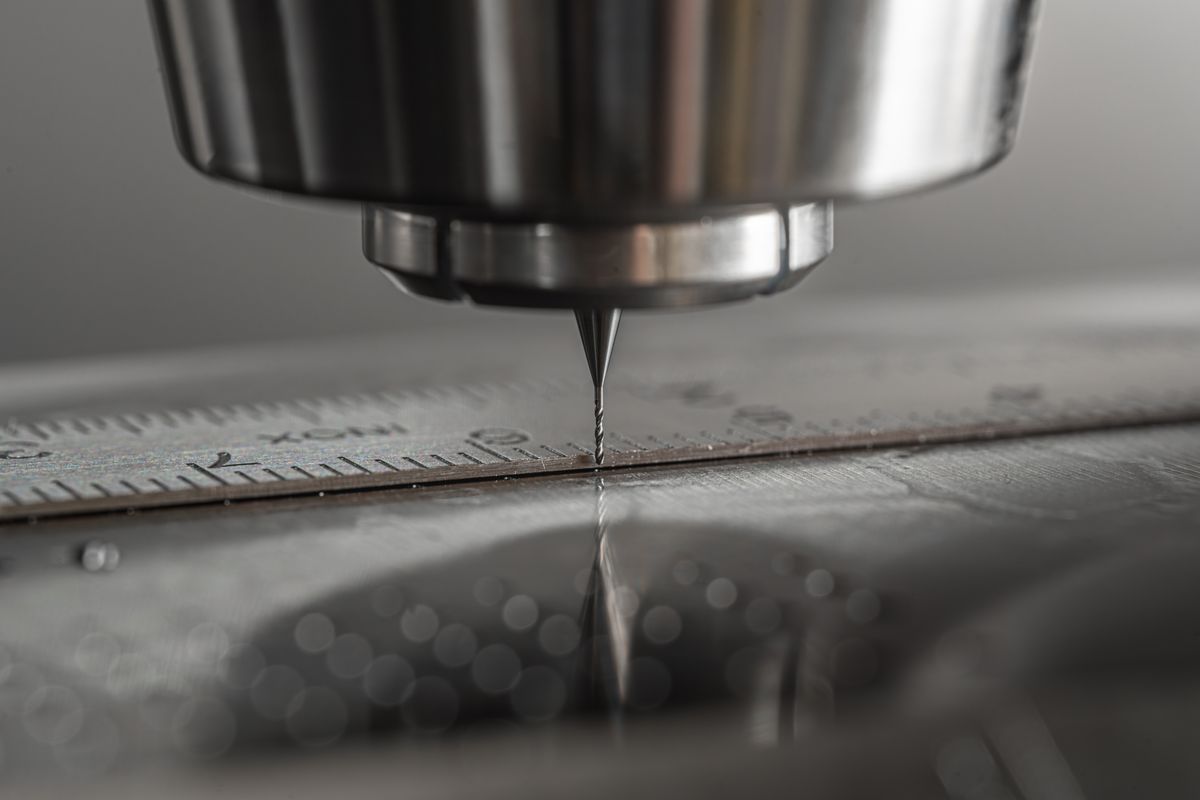
A mould is judged on two things: whether the first samples are to drawing, and whether it is still running clean two years later. Neither is settled at the design review. Both are settled by who built the tool and who is still answering the phone when it wears.
Tooling, machining, EDM, fitting and trial shots all happen here. A change to the gate or the ejector layout is a conversation with the toolmaker, not a purchase order to a third party.
What we make here
Typical work: tooling for parts we also mould, so the trial shot and the production run are the same team's problem.
How the work runs
Materials, equipment and inspection
P20, 718, H13, S136 and NAK80 mould steels, with hardened inserts where wear is concentrated. Standard components from established suppliers, so spares are available years later.
Milling, grinding, wire and sinker EDM and fitting under one roof. Tool dimensions checked on the CMM; the real inspection is the trial shot, measured against the drawing.
Capacity
| Feature | Range | What to know |
|---|---|---|
| Max mould base | 800 × 600 mm | Larger quoted with an outside base supplier |
| Cavity tolerance | ±0.01 mm | ±0.005 mm on sealing and shut-off faces |
| Cavity steels | S136, H13, 718, NAK80 | Stainless for corrosive plastics, H13 for abrasive fills |
| Cavities | 1–64 | Above 16 cavities the runner balance needs simulation |
| Lead time | 4–8 weeks | Slides and hot runners sit at the top of that range |
| Trials | T1 plus corrections | Sample and report supplied before shipment |
A mould is quoted on the part, not on the tonnage. Wall thickness, draft and the finish on the visible face decide the steel, the cavity count and the lead time.
Parts we have machined
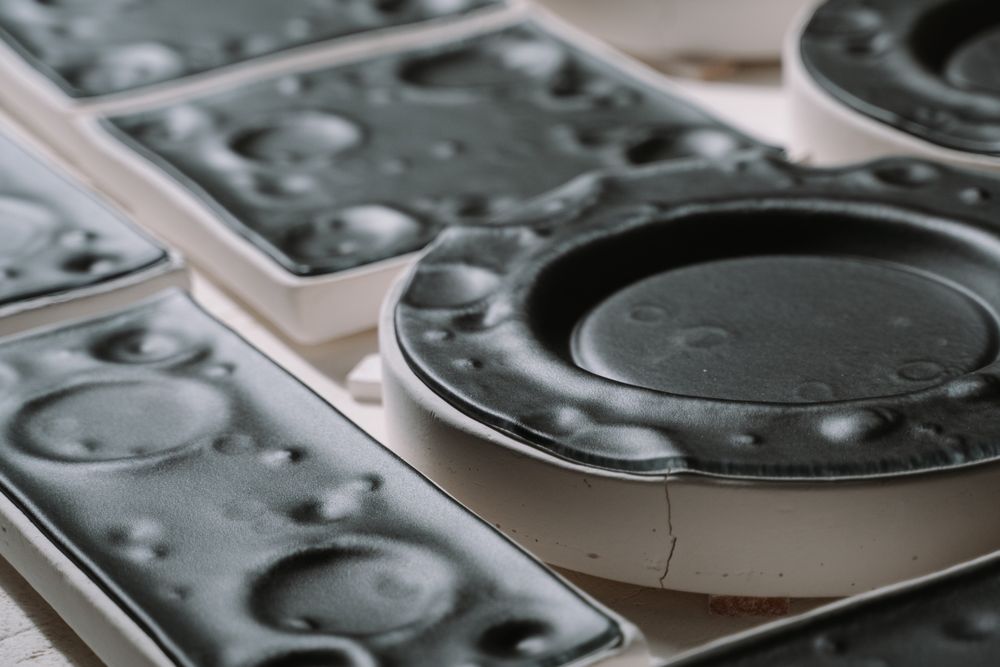
Where the money goes
Straight answers
Cavity count, slider work and steel choice move the date more than part size does. Send the drawing and the annual quantity and we will give a lead time with its assumptions written down.
Often, yes — after we inspect it. Sometimes the honest answer is that modifying it costs more than the parts it makes, and we will say so before you spend.
We can, and most customers prefer it. Storage, maintenance and refurbishment then sit inside the relationship instead of becoming a separate negotiation.
Keep reading
Request a quotation
Tell us the part, the material and the quantity. An engineer reviews your drawing and replies within one working day — usually with a suggestion on how to make it cheaper.