Gear Hobbing & Shaping
Spur, helical and internal gears cut on hobbing and shaping machines, with the mating part made in the same batch.
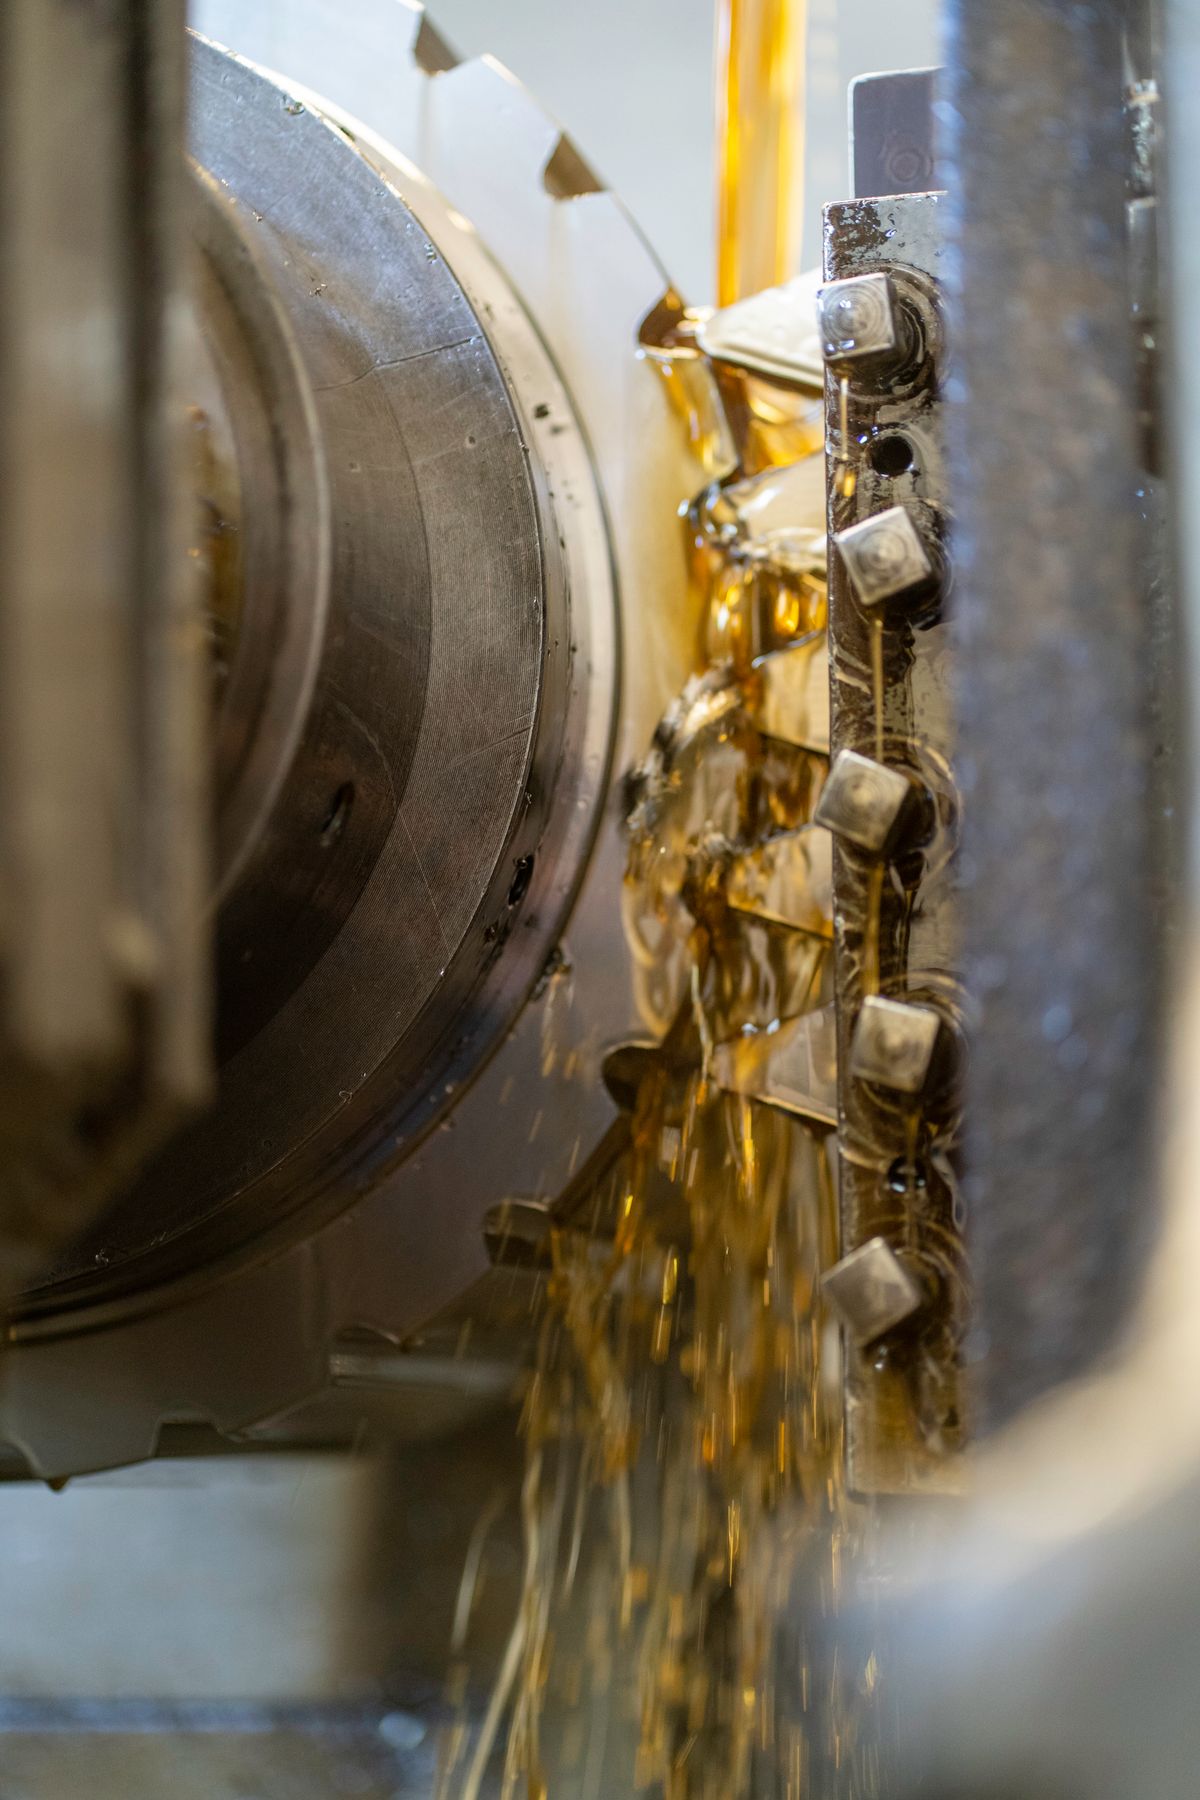
Spur, helical and internal gears cut on hobbing and shaping machines, with the mating part made in the same batch.
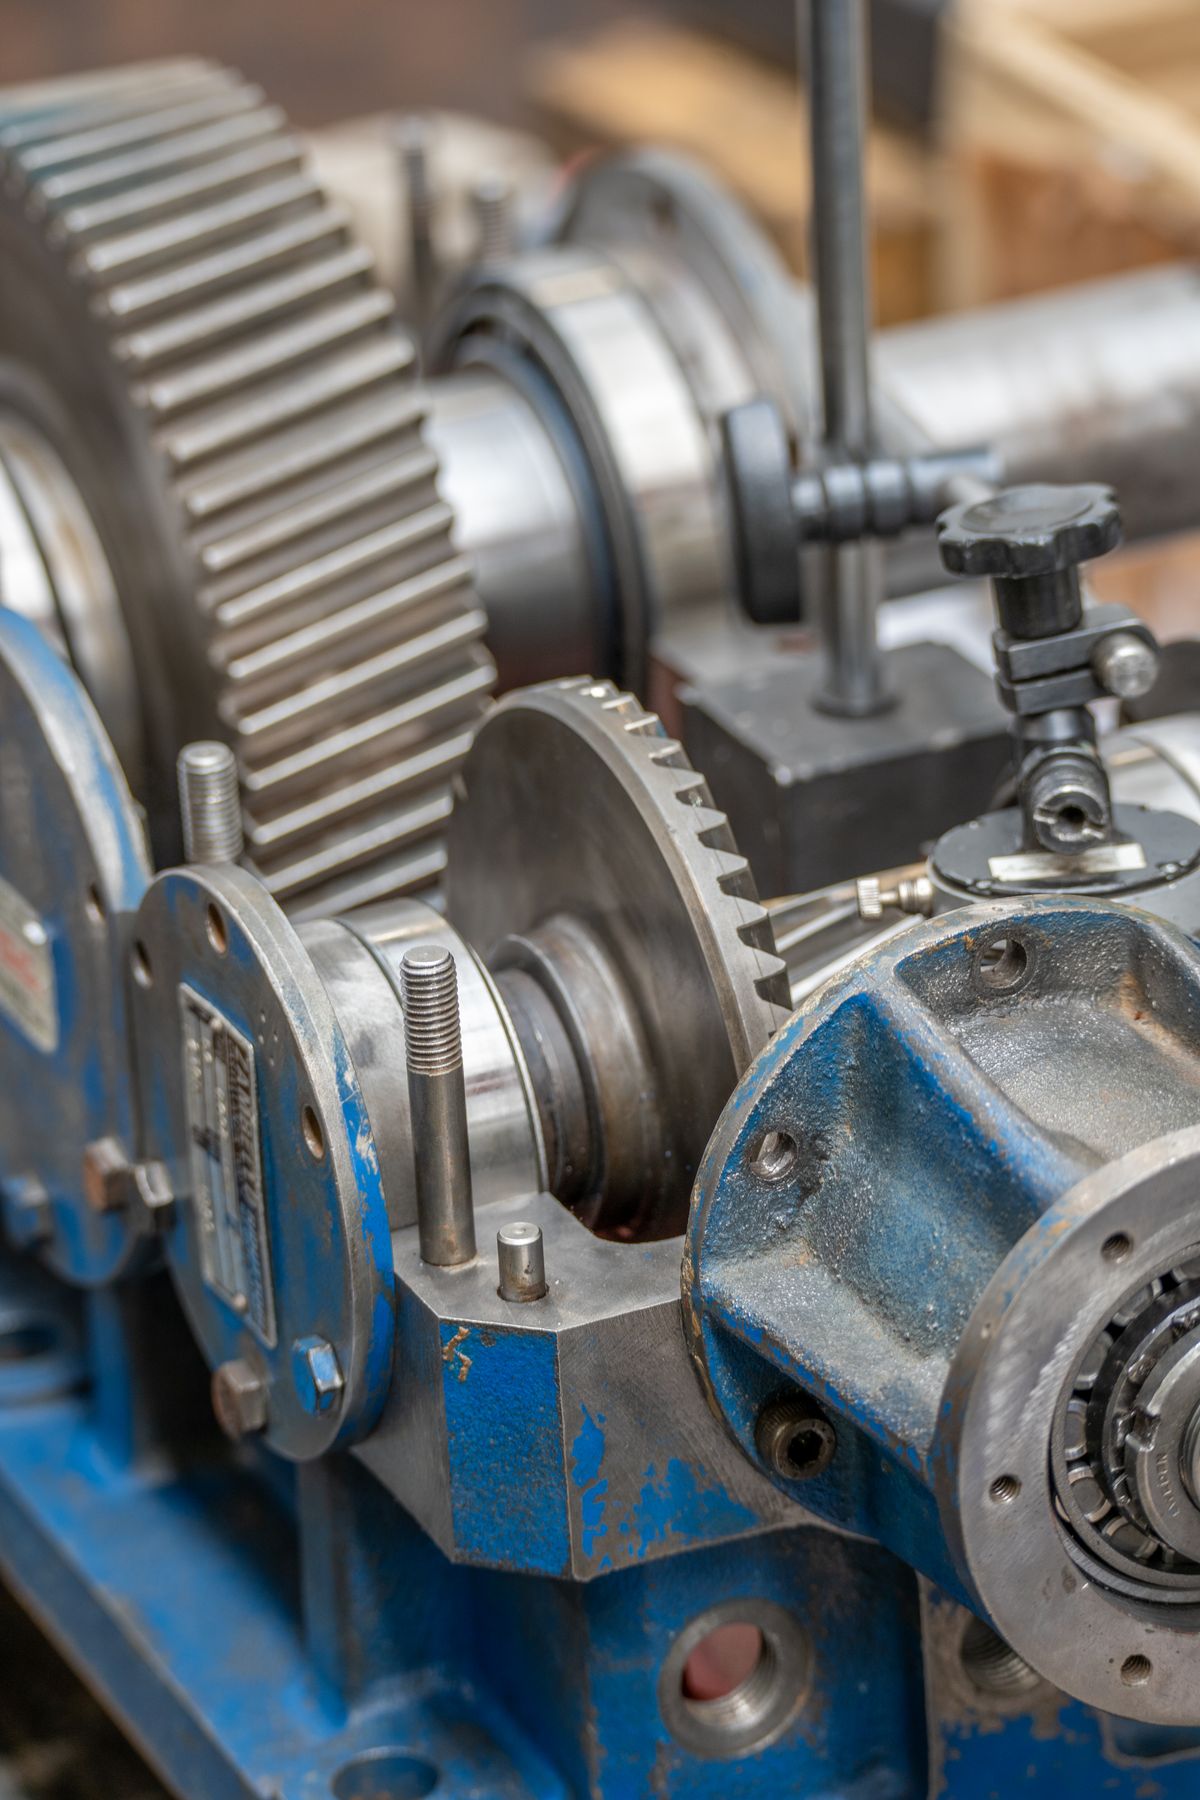
A gear is judged on how it runs against the part it meshes with, not on how it measures alone. So the pinion and the wheel are cut in the same batch, on the same machine, from the same material lot wherever the quantity allows.
Hobbing covers external spur and helical teeth efficiently. Shaping reaches internal teeth, shoulders and positions where a hob cannot run out. Where the drawing calls for hardened teeth, the part goes to heat treatment and comes back to the grinder in the same building.
What we make here
Typical work: paired sets where backlash and contact pattern matter more than the tolerance on a single tooth.
How the work runs
Materials, equipment and inspection
20CrMnTi, 42CrMo, 40Cr, 4140, 1045, stainless and brass — with case hardening and nitriding through established heat-treatment partners, and the grind after hardening done here.
CNC gear hobbing and shaping machines, with tooth profile and lead checked on the gear measuring instrument. Contact pattern checked against the mating part, not only on the chart.
Capacity
| Feature | Range | What to know |
|---|---|---|
| Module | 0.5–6 | Below 0.5 quoted case by case; above 6 usually shaped or milled |
| Max outside diameter | Ø400 mm | Hobbing; internal gears limited by the shaping stroke |
| Tooth forms | Spur, helical, internal, splines, timing | Worms and bevels are not cut in-house |
| Quality | DIN 6–8 | DIN 6 needs a ground or lapped flank after hardening |
| Helix angle | Up to 45° | Above that the hob fouling is checked before quoting |
| Hardening | Outsourced | Case or induction, then bore ground here |
Send the tooth data, not just the outside diameter. A gear drawing without module, pressure angle and backlash is a guess until we recalculate it.
Parts we have machined
Where the money goes
Straight answers
Yes. Send the blank with the drawing and we will cut, deburr and inspect. If the blank is already hardened we will tell you whether shaping is still viable before you ship it.
Both. Metric module and diametral pitch are equally fine; what matters is that the drawing states which system the teeth are defined in.
The pair is cut to the centre distance on the drawing and checked for contact pattern. Where backlash is given as a range we aim at the middle and report the measured value.
Keep reading
Request a quotation
Tell us the part, the material and the quantity. An engineer reviews your drawing and replies within one working day — usually with a suggestion on how to make it cheaper.