Automation Equipment
Machine components, gearbox parts and drive elements for equipment builders.
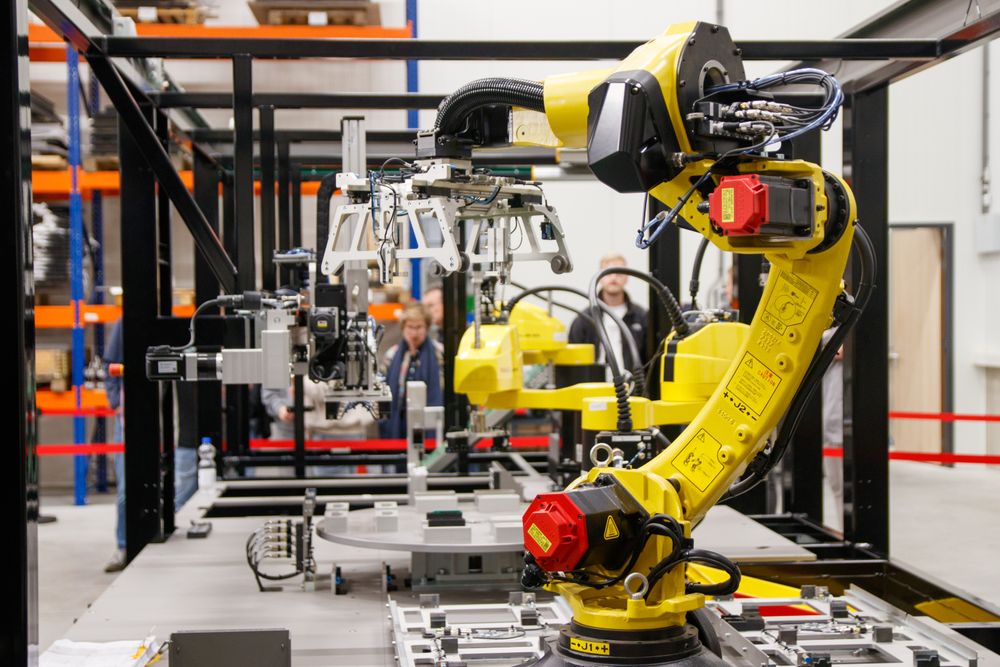
Machine components, gearbox parts and drive elements for equipment builders.
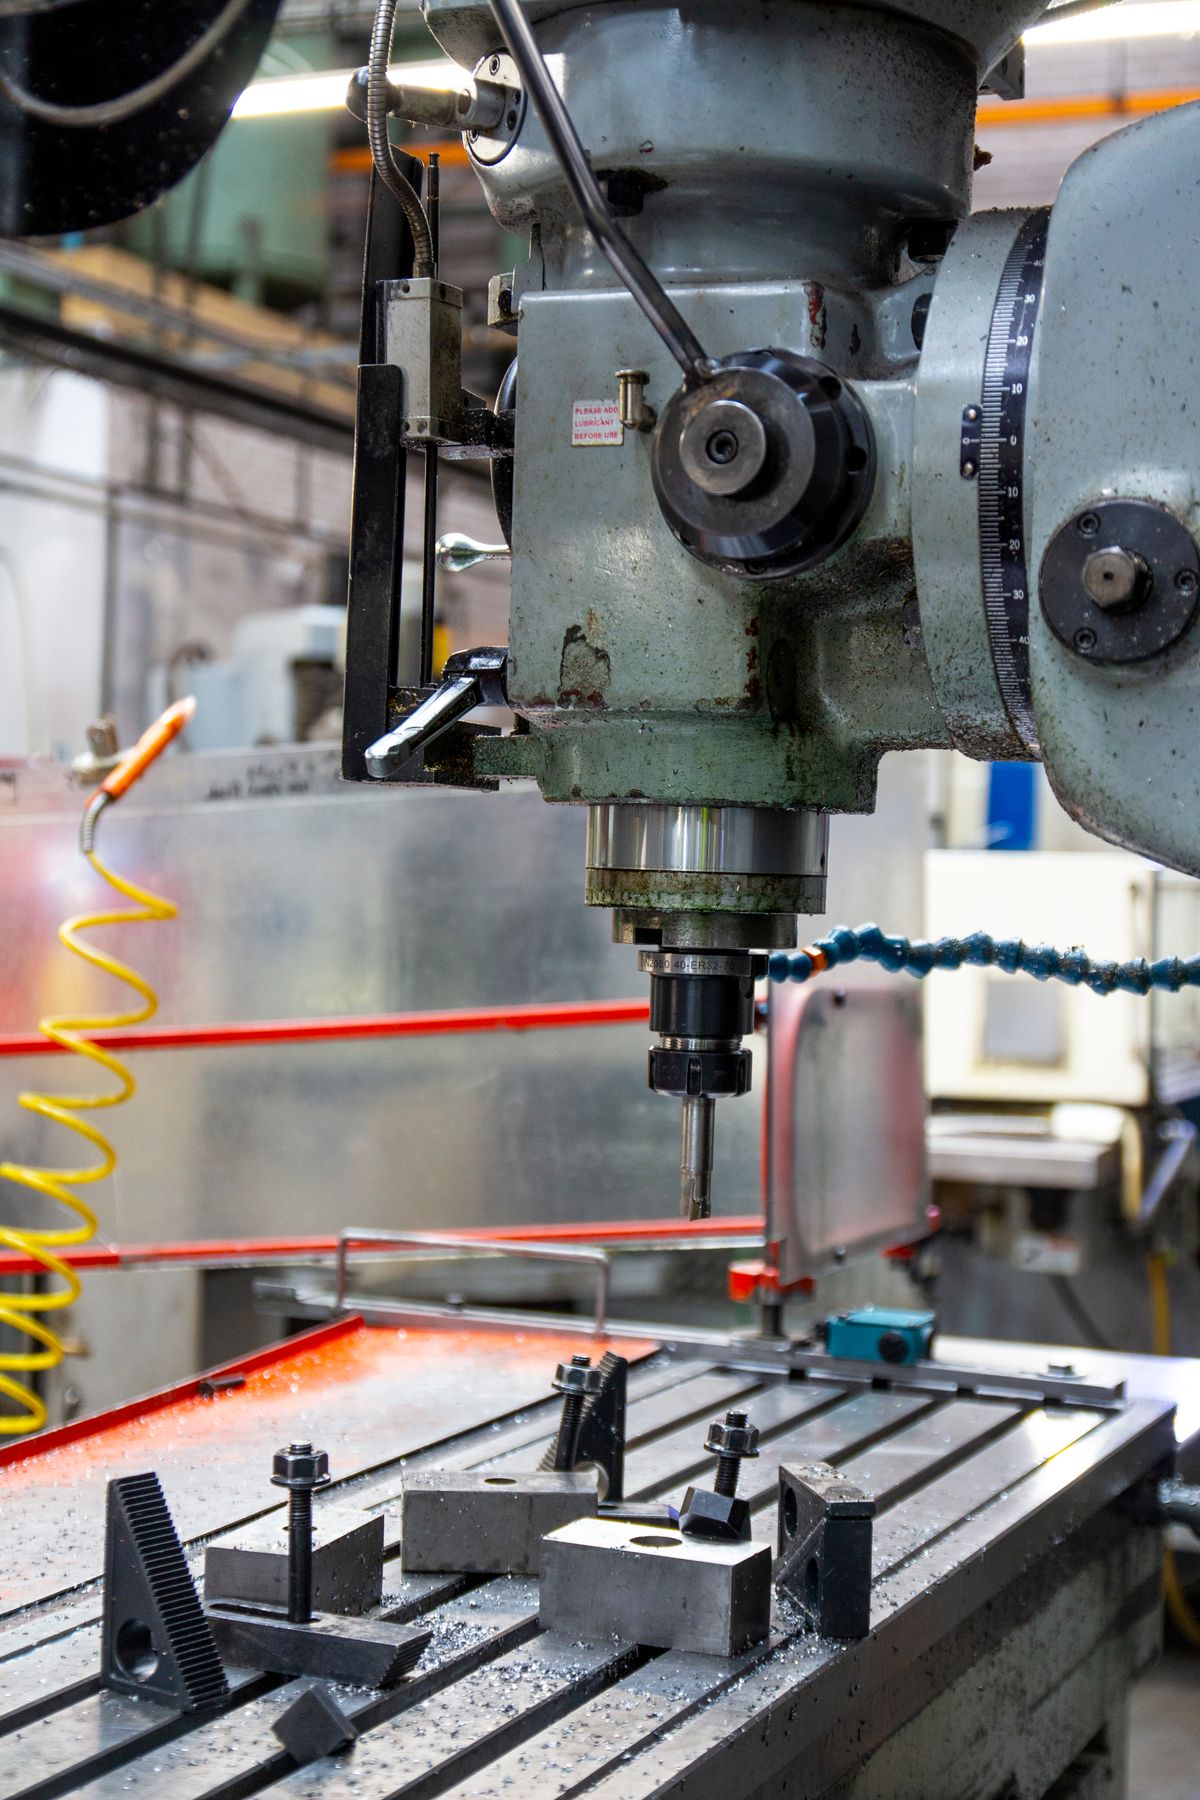
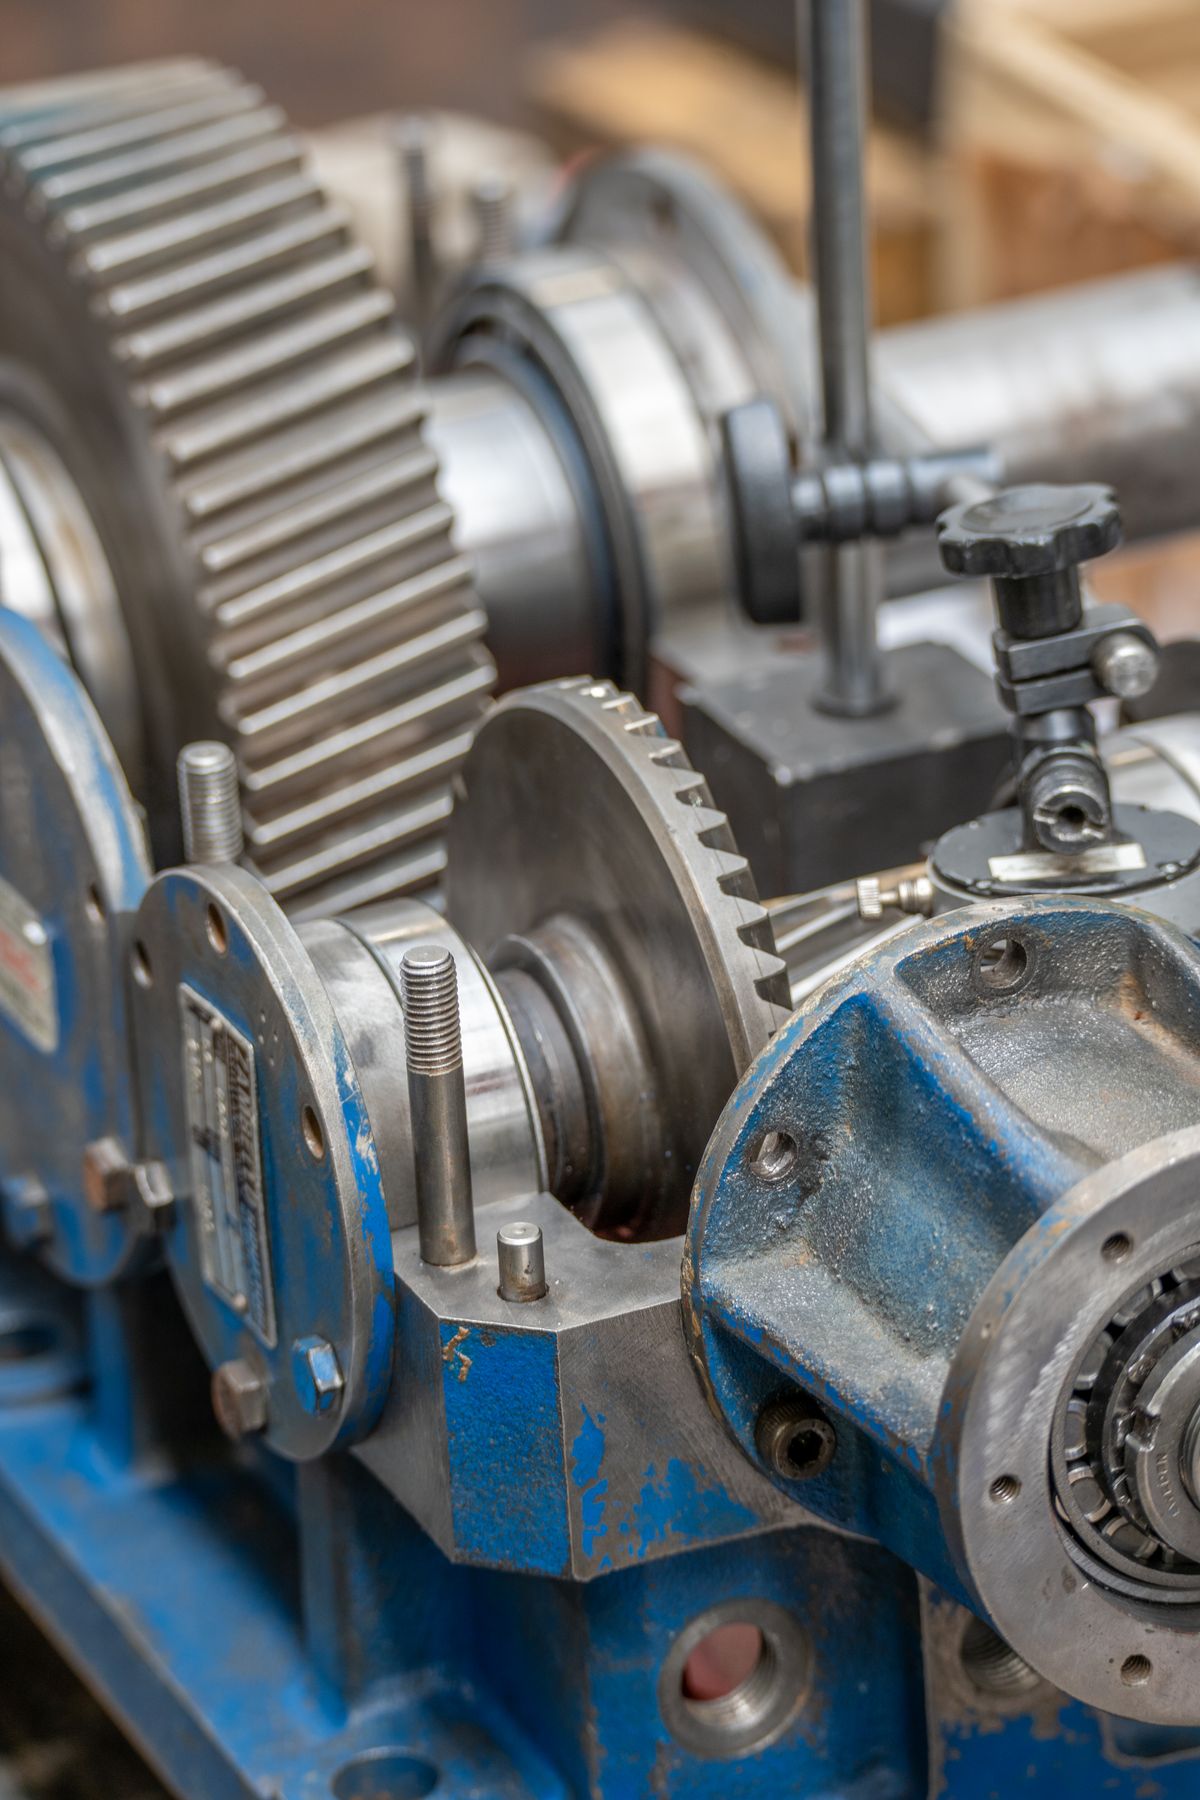
Equipment builders do not buy one part, they buy a kit that has to fit together on an assembly line. What matters in a supplier here is not the cheapest bracket. It is parts that arrive to drawing, in the right order, and do not stop the build.
We make linear-axis components, gearbox housings and shafts, pulleys, couplings, mounting plates and sensor brackets — usually as repeat batches against a drawing that has already been through several revisions.
What we make here
Typical work: repeat batches where the second order has to measure the same as the first.
How the work runs
Materials, equipment and inspection
6061 and 7075 aluminium, 1045 and 4140 steel, stainless, brass and engineering plastics. Anodising, blackening and zinc plating arranged to the drawing's finish callout.
First-article inspection on the first part of every run, CMM for hole position, and dimensional reports with measured values on request.
Capacity
| Part family | Typical material | What decides the price |
|---|---|---|
| Linear axis and rail mounts | 6061, 7075 | Flatness, hole position and anodising class |
| Gearbox housings and covers | ADC12, 6061 | Bore tolerance and sealing faces |
| Drive shafts and couplings | 4140, 303 | Concentricity and keyway or clamp detail |
| Sensor brackets | 6061, 304 | Quantity and finish; usually a laser or milled part |
| Robot end effectors | 7075, 6061 | Weight, stiffness and multiple setups |
| Conveyor and frame parts | Steel, aluminium | Length and tolerance; often a cut-and-drill job |
Automation parts fail on the interface, not on the part. Give us the mating part or the assembly tolerance and the stack is checked before the first chip.
Parts we have machined
Where the money goes
Straight answers
Yes, and that is the point of the fixture. The setup, the program and the inspection plan stay with the job, so a reorder runs on a proven process instead of being re-engineered.
Where it helps the build, yes — pressing, pinning and light assembly are quoted as a step, with the fit checked before the parts are packed.
The revision on the drawing is the revision we machine. If a new revision arrives mid-run we stop and confirm before cutting anything further.
Keep reading
Request a quotation
Industry fit is checked before the price is argued. Send the drawing with the service conditions and we will answer on both.